JBRplas Commissions HAITIAN MA6500 6500 kN Injection Molding Machine
JBRplas commissioned a HAITIAN MA6500 — 6500 kN clamping, 920 × 920 mm tie bars, 3,537 cm³ shot — expanding large-part plastic injection molding capacity.
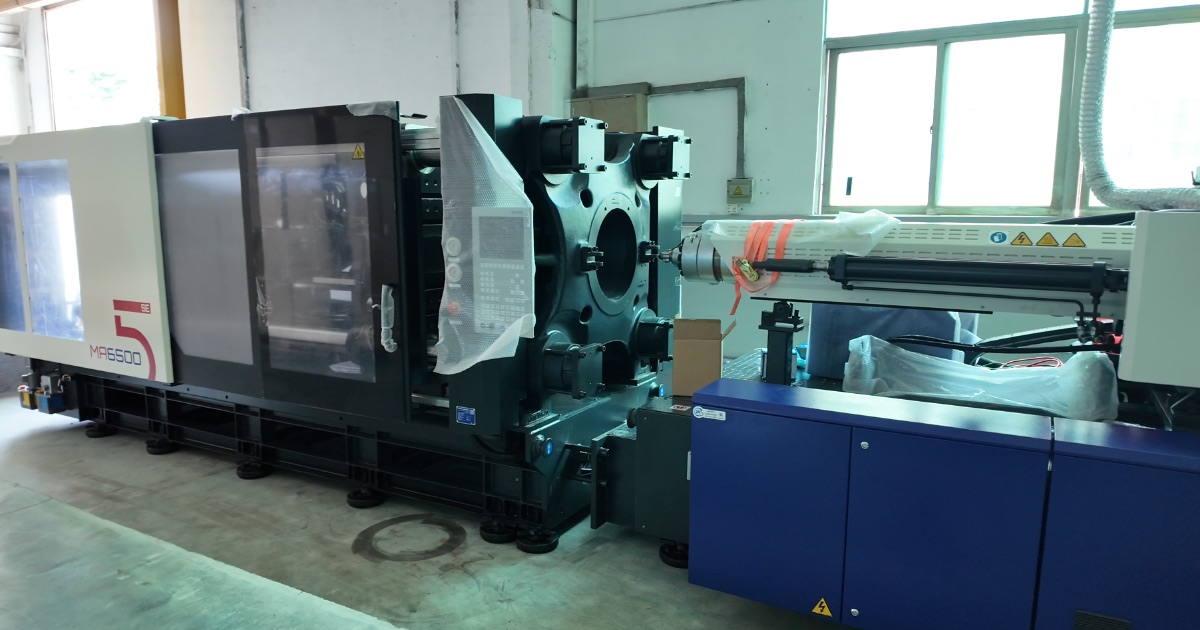
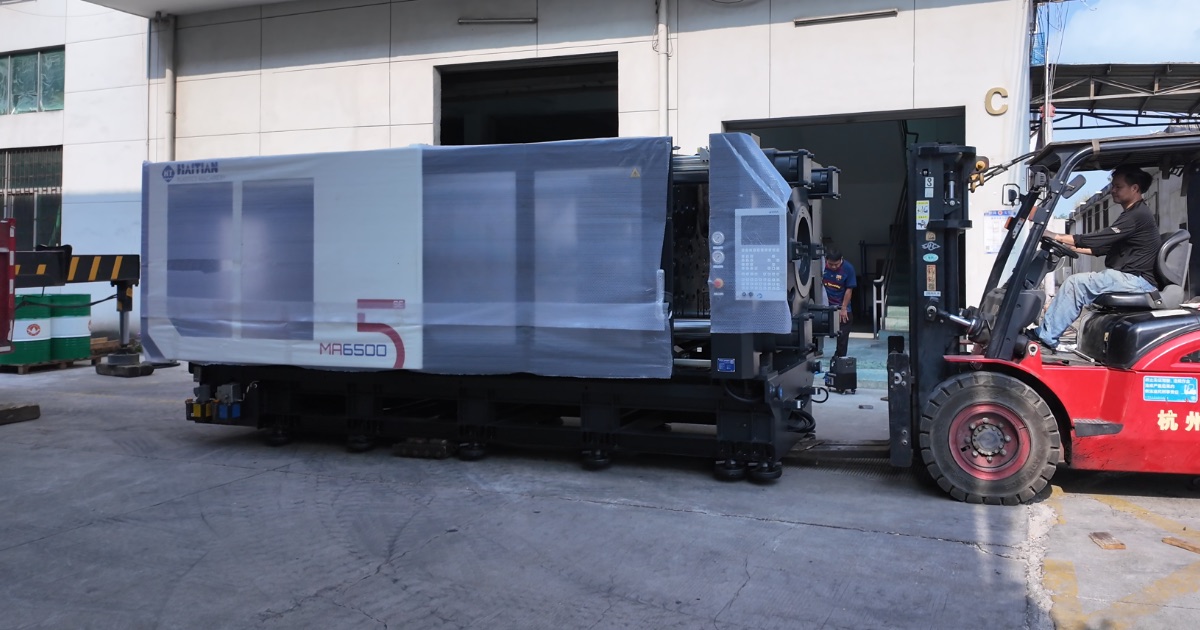
[Shenzhen, China] — JBRplas has taken delivery of a HAITIAN MA6500 injection molding machine at its Shenzhen facility on 14 October 2026. Installation and commissioning are complete and the machine is now in production.
The MA6500 is a 6500 kN (≈ 650 t) machine with 920 × 920 mm tie-bar spacing, a mold stroke of 900–970 mm, and it accepts molds from 400 to 900 mm in height. Maximum theoretical shot volume is 3,537 cm³, which corresponds to roughly 3,188 g in polystyrene.
Machine Specification
| Parameter | HAITIAN MA6500 |
|---|---|
| Manufacturer | HAITIAN |
| Clamping force | 6500 kN (≈ 650 t) |
| Tie-bar spacing | 920 × 920 mm |
| Mold stroke | 900–970 mm |
| Mold height (min–max) | 400–900 mm |
| Max. theoretical shot volume | 3,537 cm³ |
| Max. shot weight (PS) | 3,188 g |
| Status | Installed, commissioned, in production |
What 6500 kN Covers in Practice
Clamping force sets the projected area a mold can hold shut. The relationship is straightforward: the clamp must exceed cavity pressure multiplied by the projected area of the part and runner.
At the cavity pressures typical for engineering resins, the MA6500 covers roughly the following projected areas:
| Assumed cavity pressure | Projected area the clamp holds |
|---|---|
| 300 bar (30 MPa) | ≈ 2,167 cm² |
| 500 bar (50 MPa) | ≈ 1,300 cm² |
| 800 bar (80 MPa) | ≈ 813 cm² |
These are indicative figures derived from the rated clamp force, not guaranteed process windows — the real limit depends on the resin, wall thickness, flow length and gate layout, and is confirmed during mold flow review for each program. What the numbers show is the class of part this machine is sized for: large single-cavity components and multi-cavity tools with substantial projected area, rather than small precision parts.
The 900–970 mm mold stroke matters as much as the tonnage. It is what allows deep-draw parts — tall bins, deep housings, parts with long cores — to be ejected without a special long-stroke machine, and it widens the range of existing molds that can be transferred onto this press during a tool transfer.
Products This Machine Is Sized For
Automotive Components
Interior door panel liners, centre console frames, small bumper components, fan impellers and intake manifolds. These parts share two characteristics: a projected area that smaller presses cannot hold at production cavity pressure, and a wall-thickness-to-flow-length ratio that needs consistent packing across a long flow path.
Smart Home Products
Large enclosures, hubs and docking stations with generous projected area, and multi-part housings where the cosmetic surface has to stay free of flow marks across a wide face.
Medical Device Housings
Benchtop instrument housings and diagnostic device enclosures, including parts molded in the clean room cell where the same tonnage class is required together with the environmental controls.
Timeline
| Date | Milestone |
|---|---|
| 2026-10-14 | Delivered to the Shenzhen facility and moved into the press bay |
| 2026-10-14 | Installation complete |
| Now | Commissioning complete, in production on large-part programs |
What This Means for Clients
Large parts no longer queue behind small ones. On a press line where the top tonnage is committed, large-part work waits for a window. Adding a 6500 kN machine separates that queue: large molds run on the MA6500, small and medium work keeps running on the existing machines.
Tool transfer is less constrained. The 400–900 mm mold-height range and 900–970 mm stroke mean a wider set of existing molds can be moved onto this press without modification — useful when a program needs to scale up volume without cutting a new tool.
Cavity pressure headroom for difficult resins. The tonnage reserve on a 6500 kN machine is what allows glass-filled engineering resins and long-flow parts to run at the cavity pressure the process actually needs, instead of being pushed to the edge of the clamp on a smaller press.
The full machine inventory, including tonnage, tie-bar dimensions and shot capacity for every press, is on the equipment list. For process capability by material and tolerance class, see injection molding services and capabilities.
If you have an existing mold that needs a larger press, or a new large-part program to quote, send the 3D file and the current mold drawing — we will confirm which machine the work is planned on and whether the tool needs modification before transfer. Request a quote →